
- Hotline: 0909 981 890

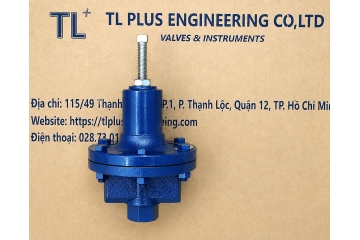
Pressure reducing valves are used for saturated steam and pressure reducing valves are used for liquid fluids
Pressure reducing valves are used for saturated steam and pressure reducing valves are used for liquid fluids

Pressure regulating valves (also known as pressure reducing valves) are crucial devices in industrial and commercial piping systems. Their primary function is to maintain a stable downstream pressure, regardless of upstream pressure fluctuations or changes in flow rate. Depending on the application, selecting the appropriate valve is essential to ensure efficient and safe operation of the valve and the entire system.
Differences in application between pressure regulating valves (pressure reducing valves) used for saturated steam systems and pressure regulating valves (pressure reducing valves) used for liquid fluid systems:
Pressure regulating valves (pressure reducing valves) for saturated steam systems: typically used to reduce upstream pressure from boilers or main pipelines before steam enters heating systems or pasteurization systems. These valves need to provide precise pressure control regardless of changing flow rate demands and fluctuating inlet saturated steam temperature.
Pressure regulating valves (pressure reducing valves) for liquid fluid systems: typically used to reduce pressure from feedwater systems, hydraulic systems, chemical treatment systems, and fuel distribution systems. These valves need to maintain a stable downstream pressure without sudden pressure increases.
Characteristics of pressure regulating valves (pressure reducing valves) used for saturated steam:
The valve and its internal components are capable of withstanding high temperatures, with a minimum operating temperature of up to 250°C. Therefore, materials such as stainless steel or special alloys are often used to prevent corrosion and thermal fatigue. The seals and valve diaphragms are made from heat-resistant materials to ensure functionality during operation. Along with a special internal design, the valve balances to respond to rapid pressure changes while maintaining a stable output pressure. The pressure regulating valve (pressure reducing valve) incorporates safety features such as a pressure reducing valve, a high-temperature spring, and a secure locking mechanism to prevent unintentional changes to the settings.
Characteristics of pressure regulating valves (pressure reducing valves) for fluid systems:
The valve and its internal components meet corrosion resistance and fluid viscosity requirements. Common materials include brass, stainless steel, or plastic composite materials, depending on the type of fluid.
Incompressibility and flow stability, fluids are incompressible, so pressure changes directly affect the mechanical forces within the valve.
Fundamental differences between saturated steam and fluid:
Saturated steam is a compressible fluid with phase changes, high temperature, and low density.
Liquid is generally incompressible and has a much higher density and significantly lower temperature than saturated steam.
The effect of condensate on saturated steam flow.
Because saturated vapor can change phase and condense into water, the design and installation process must ensure that condensate does not enter the valve body. Failure to do so can lead to hydraulic shock, damage to the pressure regulating valve, or interruption of pressure control.


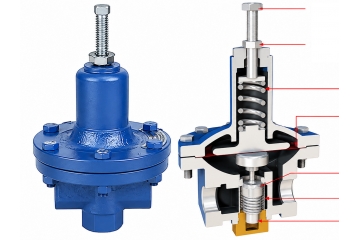
Pressure Reduce valves Seri O Watson McDaniel Pressure Regulator valves Seri HD Watson McDaniel
If you are experiencing any of the pressure regulating valve problems listed below, please contact us for advice on solutions.
TL Plus Engineering specializes in consulting on system and equipment improvements, and calculating energy recovery for saturated steam systems.
If you need to improve your saturated steam pressure reducing valve system, please contact us via email sales(at)tlplus-engineering.com
TL Plus Engineering is the authorized distributor of Watson McDaniel products in Vietnam and other Asian countries.
Some types of saturated steam pressure reducing (regulating) valves are available.




Related posts
-
![Advantages of inverted bucket steam traps compared to float-type steam traps]()
When you need a steam trap with high water hammer resistance, durability in high-pressure systems, and reliable operation under conditions of severe impact or surge loads.
-
![How Does a Direct Pressure Reducing Valve for Saturated Steam Work?]()
At startup, the pressure regulating bolt is in the loosen state, the inlet steam pressure and the valve seat spring are in the closed state. We begin by turning the pressure regulating bolt on top of the valve clockwise. The bolt moves linearly, pushing the spring downwards, simultaneously lowering the valve diaphragm, controlling the valve to open, and the fluid and outlet pressure begin to increase. The pressure inside the valve body pushes the diaphragm upwards, balancing the spring force. The pressure after the valve increases simultaneously until it reaches the set pressure value, at which point the valve begins to close gradually, preventing the pressure after the valve from exceeding the set threshold.
-
![FLASH STEAM RECOVERY]()
When the pressure of saturated condensate is reduced, a portion of the liquid “flashes” to low-pressure steam. Depending on the pressures up stream, the flash steam contains normally 3% to 50% of the energy content of the original condensate. Almost cases, condensate receivers the flashing steam is vented to atmosphere and its energy content lost.
-
![WHAT IS STEAM ?]()
-
![WHY USE STEAM?]()
There are three main forms of energy used in industrial processes: electricity, direct heat, and steam.
-
![SATURATED STEAM TABLE]()
-
![]()
-
![WHY NEED EVAPORATOR ?]()




Copyright © 2020 Technical TL +